Konya / Karatay
Ask for Price
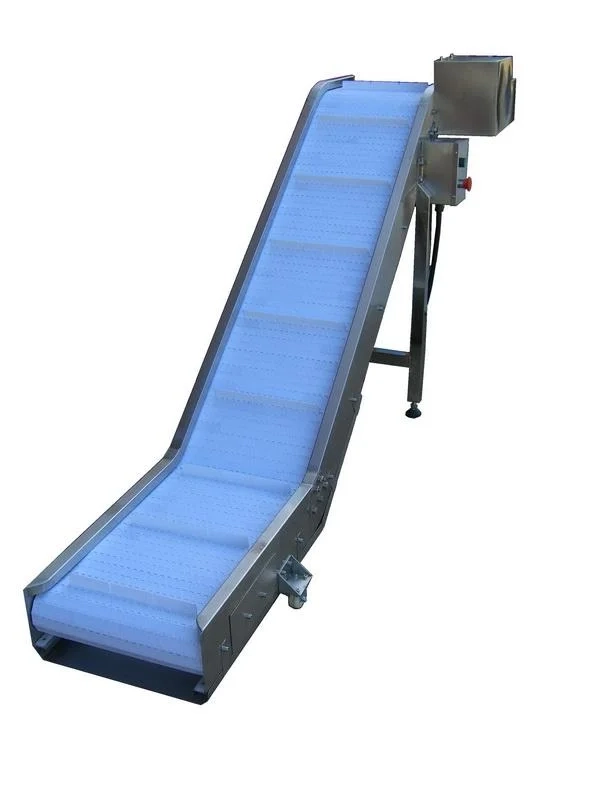
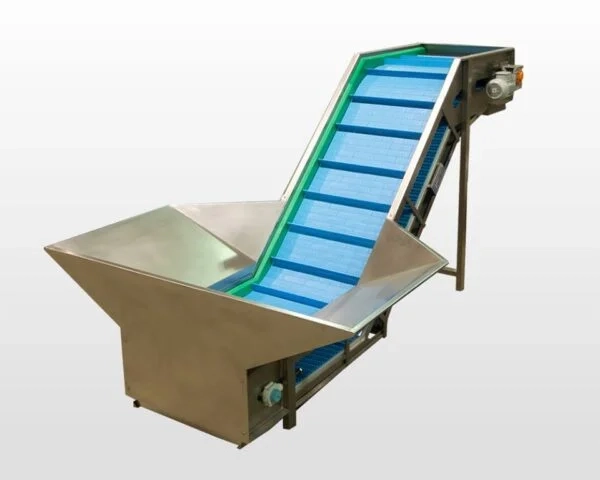
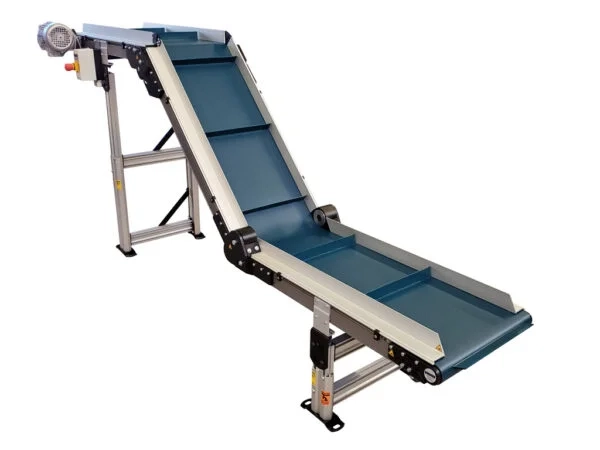
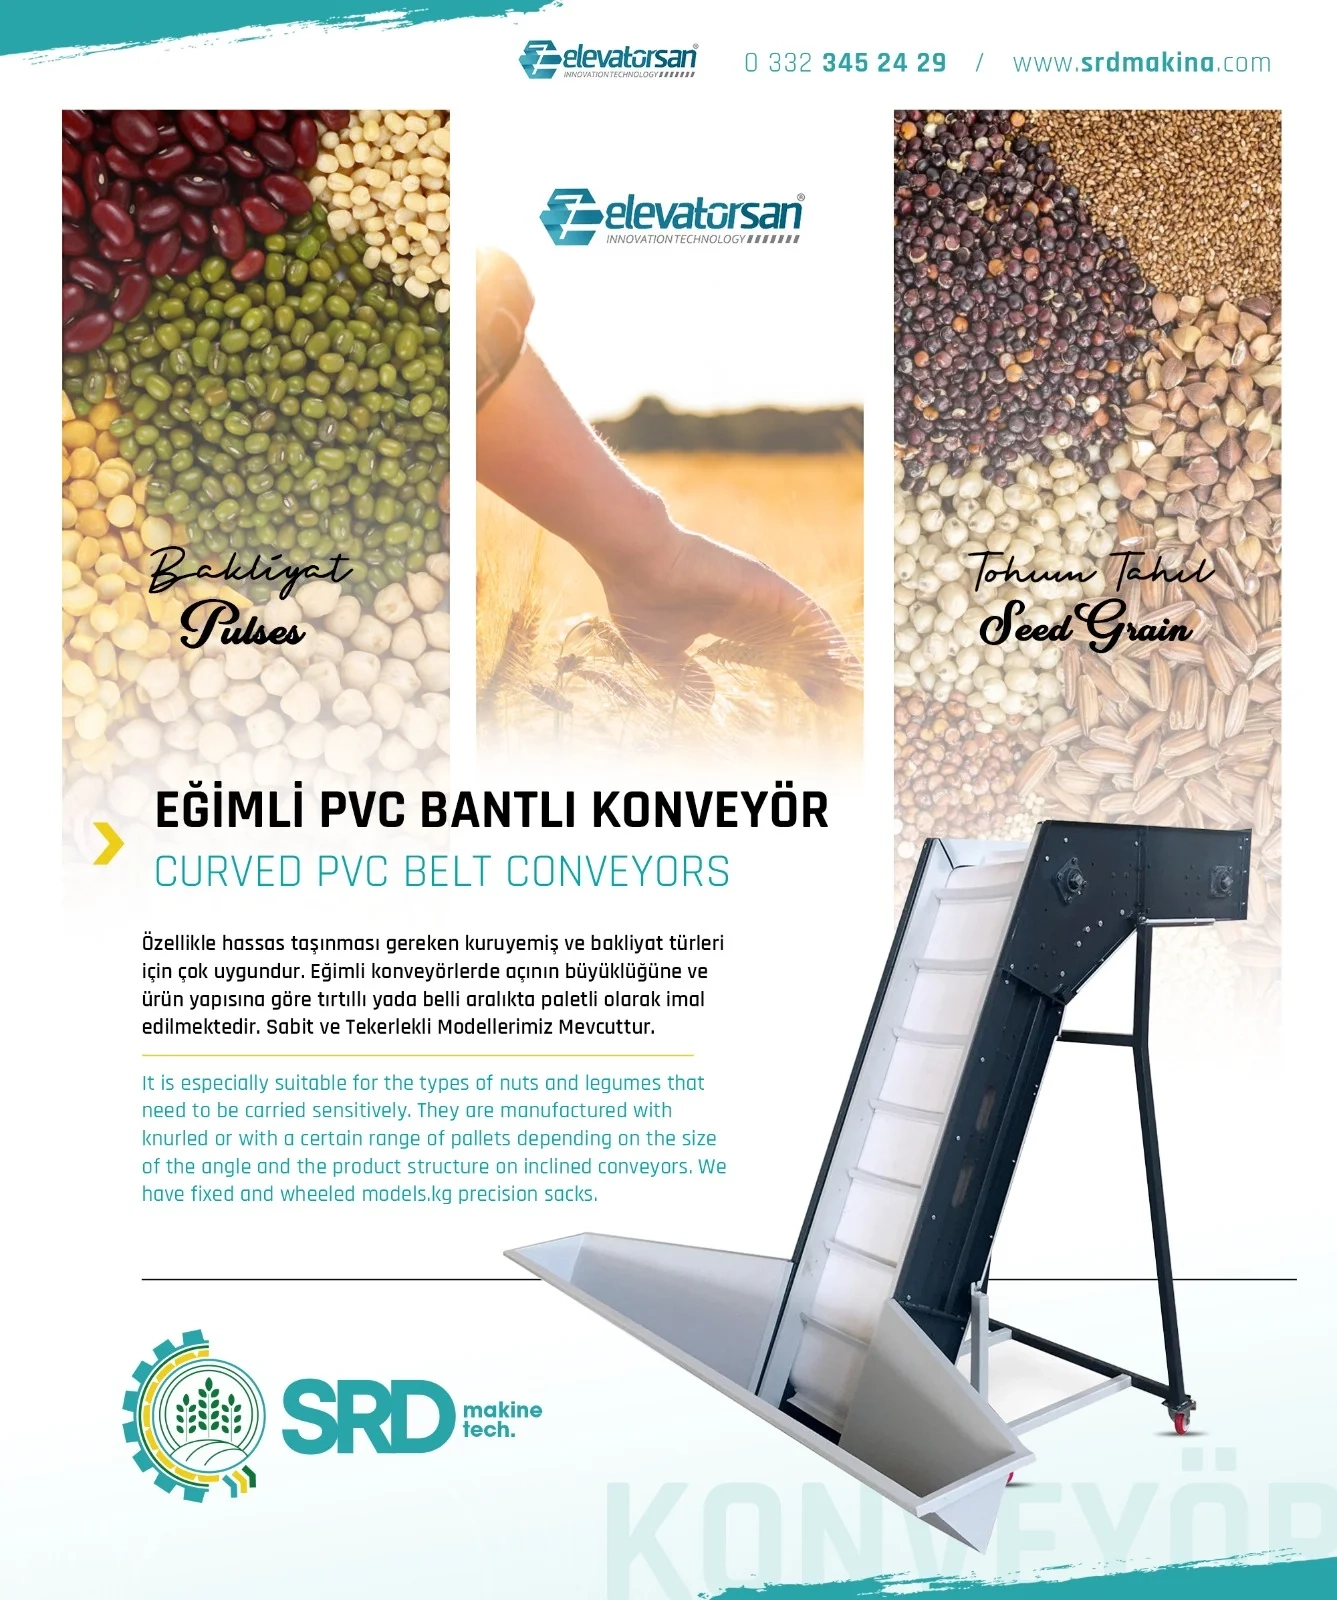
Inclined Conveyor is a high-strength conveying system designed to transfer bulk, powder, granular, or packaged industrial products—including mining, chemical, recycling, agricultural, logistics, and food products—safely, continuously, and without damage between different elevations or floors at a defined incline angle, either upward or downward.
Working Principle: The system operates by using drums driven by a powerful motor-reducer assembly to move the conveyor belt in a linear and inclined loop:
Inclined Conveying and Anti-Slip Design: Special profiles, cleats, or chevron flight structures are used on the belt surface to prevent bulk materials or packages from sliding backward on steep inclines. This ensures stable, loss-free flow even at steep angles.
Industry-Specific Frame and Belt Options: In heavy industry, mining, and logistics applications, static oven-painted steel (St-37) frames with high impact resistance and thick rubber/PVC belts are preferred. For processes such as chemical, pharmaceutical, and food applications requiring high corrosion resistance and hygiene standards, AISI 304/316 stainless steel construction and modular/PU belt alternatives are used.
Process Automation and Flexible Integration: Depending on the facility layout, the conveyor can be designed with a straight inclined, swan-neck (L- or Z-type), or telescopic frame. It minimizes the need for manual labor by fully automating the feeding of raw materials from storage areas to production lines, vertical transfers between process units, and the loading of packaged finished products onto shipping and transport vehicles.