Konya / Karatay
Ask for Price
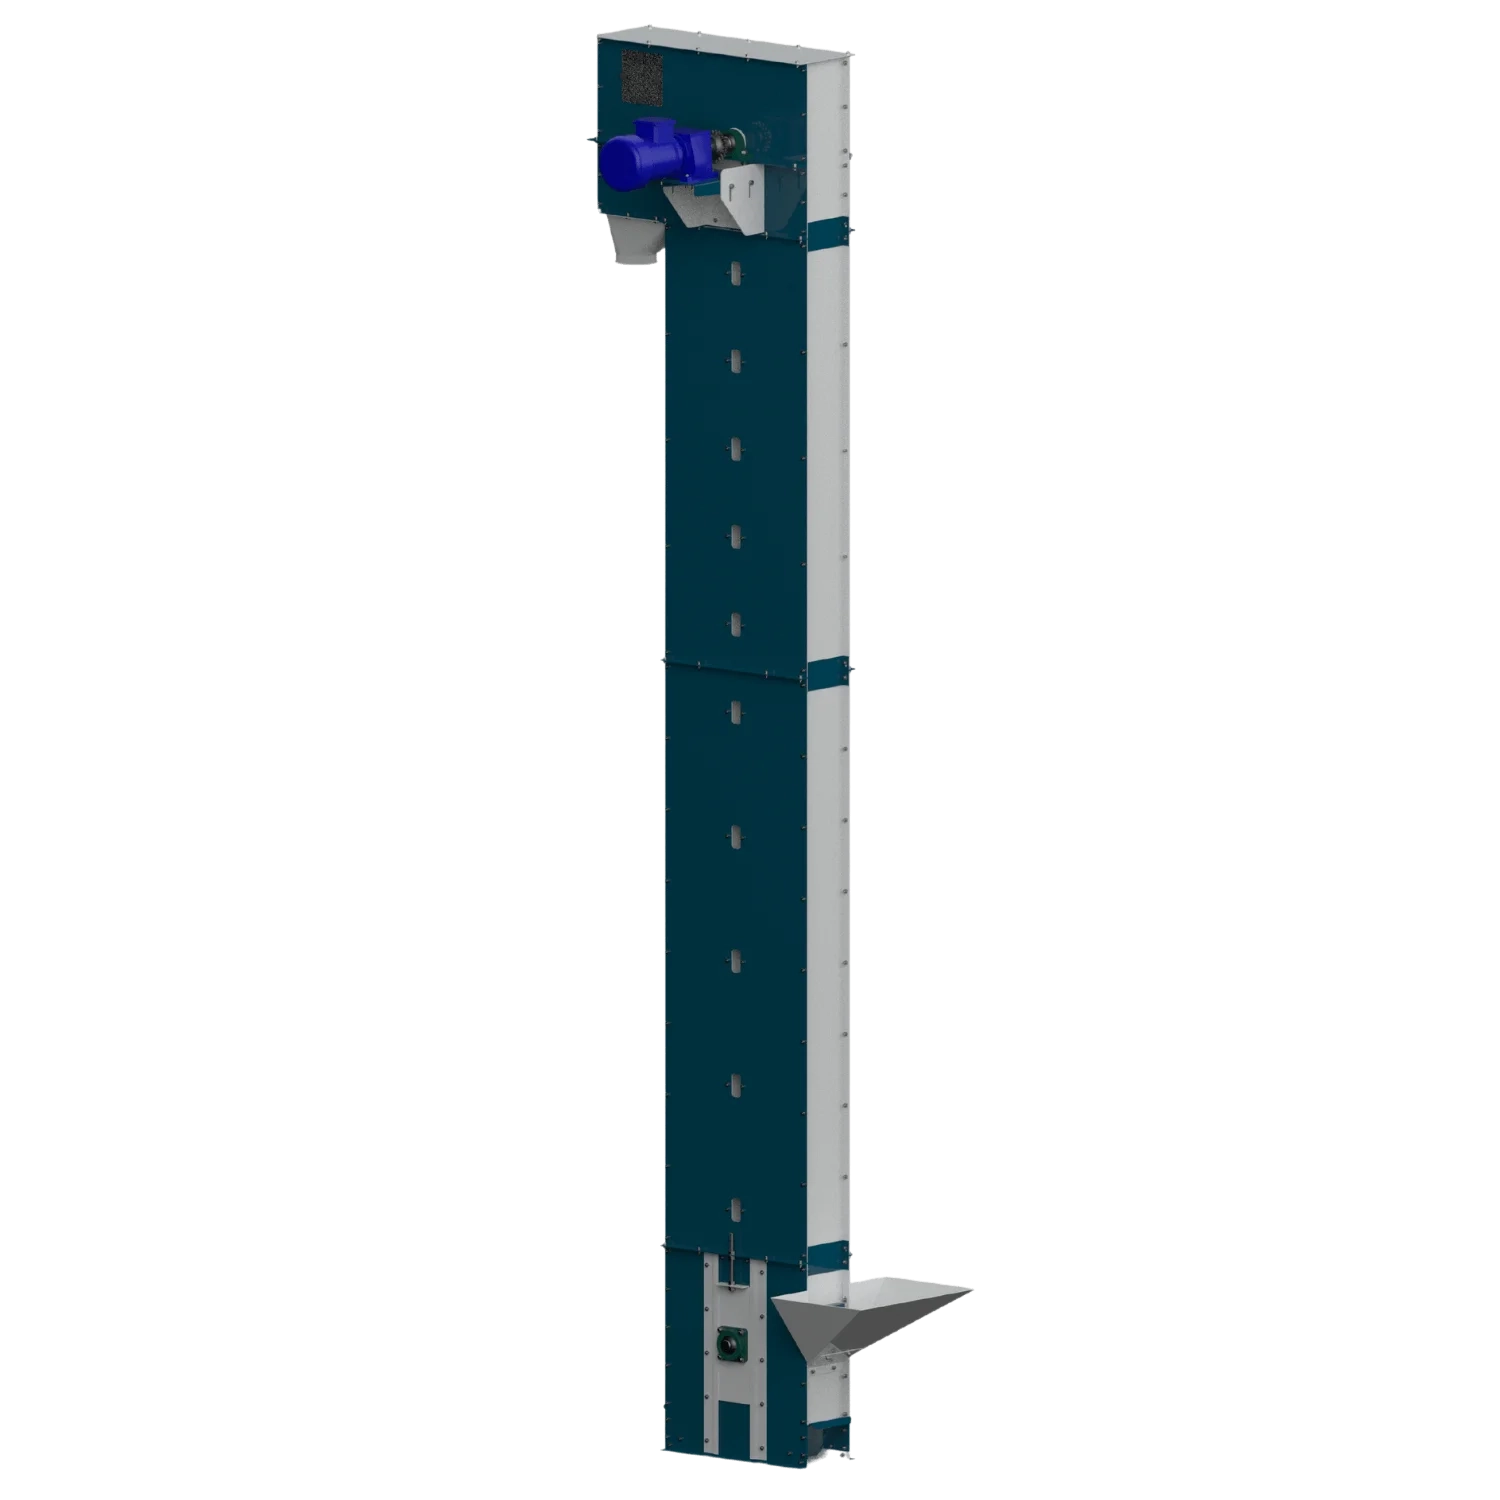
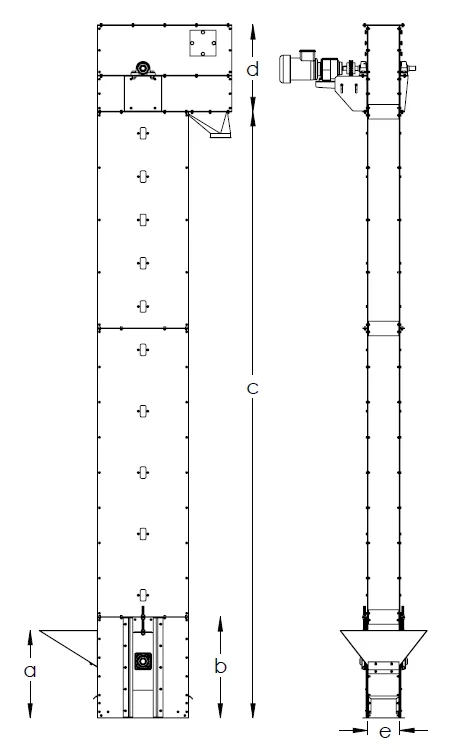
Vertical Bucket Elevator is a high-capacity vertical conveying system designed to safely transport large quantities of bulk and granular materials that are not highly sensitive to breakage, such as dust, flour, wheat, barley, corn, and granules, along a completely vertical (90°) conveying route.
Operating Principle: The system operates by scooping bulk material from the lower body and conveying it upward using metal or plastic buckets mounted on a high-strength belt rotating between the machine's pulleys. At the upper head section, the material is discharged by being thrown into the discharge chute through the effect of centrifugal force:
High-Speed Discharge by Centrifugal Force: When the buckets, rotating in synchronization with the belt speed, reach the top point, the centrifugal force generated transfers the material inside the buckets to the discharge outlet within seconds. This provides maximum efficiency in high-volume vertical conveying applications.
Robust Casing-Type Body and Galvanized Construction: A corrosion-resistant galvanized coating is combined with a rigid casing-type body design that provides high resistance to harsh environmental conditions. Long-life metal or industrial plastic bucket options are available depending on the required wear resistance.
Fully Enclosed Dust-Tight System: For environmentally friendly and safe operation, the elevator body is manufactured as a fully enclosed system. It effectively prevents dusty materials such as flour, feed, and grain from escaping into the surrounding environment and minimizes product loss.
Modular Bolted Construction: The fully bolted modular construction makes on-site installation, transportation, and periodic maintenance extremely easy. When the plant capacity or layout changes, the system dimensions can be easily modified, and the buckets can be practically replaced or adapted with different volumes.